Combination Inspection Systems Integration
Plan mechanical, electrical, control, data, safety and operator interfaces for combination inspection systems.
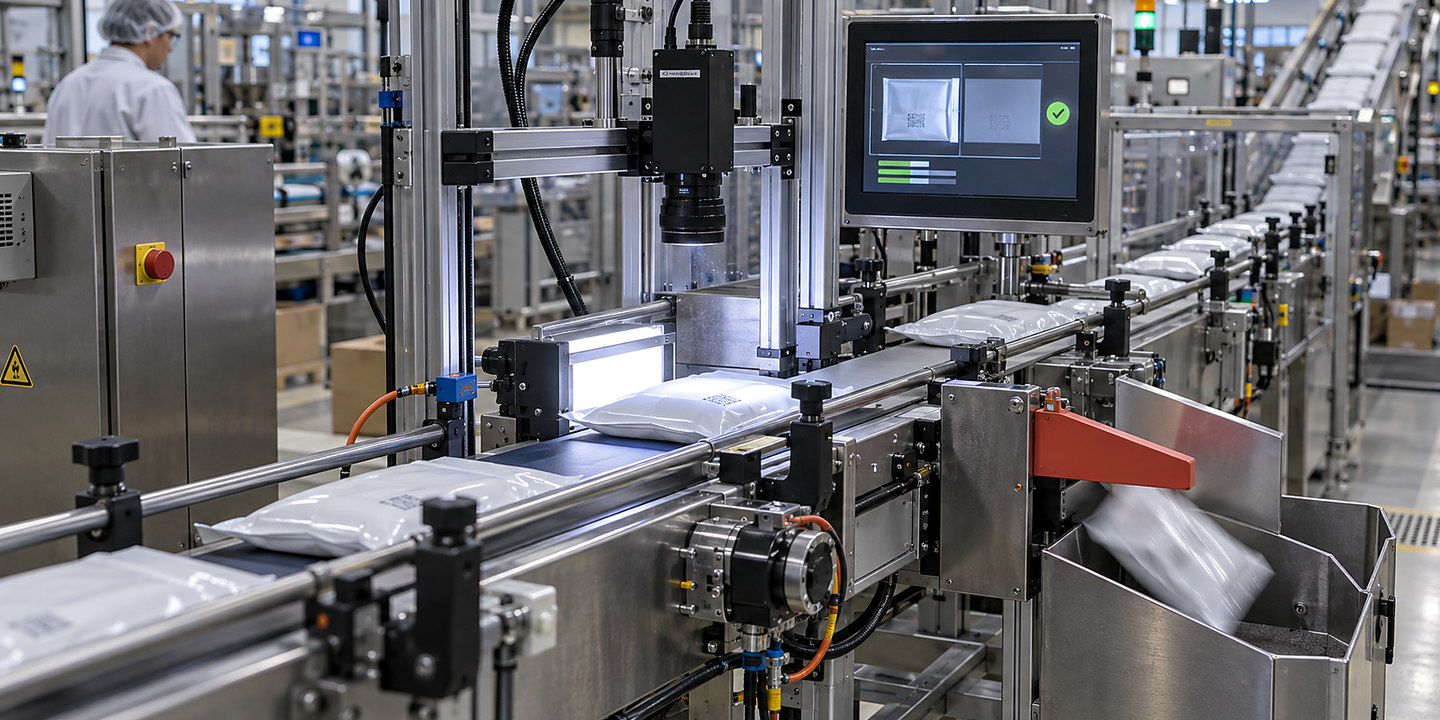
Photographs illustrate general inspection equipment. Combined vision, code and weight performance must be established with representative packs and the complete result and reject sequence.
Map pack presentation and result timing across all inspection stages. Define recipe data, pack tracking, reject responsibility and the response when one required result is absent or disagrees with another.
For retrofit or multi-variant checks involving combined vision, code and weight inspection, define every physical connection, signal, responsibility, check and fallback before installation.
Connect equipment, controls and people into one reliable process — Combination Inspection Systems
Plan combination inspection systems around representative good, bad and marginal samples, line presentation, lighting, reject handling and challenge criteria. Discuss an optical feasibility trial with Oxford Vision Systems. Your integration review should connect part presentation and production speed, optics, lighting and environmental conditions and the people who run the process.
Discuss your application

Combine inspection results without losing pack identity
A combined vision, code and weight system should make a defined decision for one physical pack. Start by drawing the order of stations and the decision deadline at the reject point. Sharing a conveyor does not, by itself, show that several results belong to the same pack.
Assign one result set to each pack
Agree how a pack is identified when it enters, how position is tracked between stations and how that identity is retired after the final decision. Include conveyor transfers, slip, gaps and a pack removed by an operator. Keep separate states for a passed check, a failed check and a check that did not return a usable result.
Write the decision rule before wiring outputs
List mandatory checks for each product recipe. For example, a hypothetical recipe might require correct artwork, matching lot text and weight within its approved limits; a failure or unavailable required result leads to the agreed hold or reject route. An optional diagnostic image should not silently become a mandatory release check. The responsible quality team should approve these distinctions.
Allow for different result arrival times
The code reader may finish before the camera, while weighing occurs at another conveyor position. Define when results become final, how late results are handled and what happens if a station is disconnected. Challenge the complete sequence at the intended pack spacing and through stops; average processing time alone does not prove that the slowest required result arrives before rejection.
Control recipe changes across every station
Keep product identity, expected code values, vision recipe and weighing setup coordinated. Decide how mismatched versions or incomplete changeovers are detected before packs are released. Record who may change each setting and retain an agreed recovery procedure for a failed update, rather than allowing each instrument to resume independently.
Prove rejection and fault recovery together
Test adjacent failed packs, a reject mechanism that does not complete its action, and a missing confirmation. Then stop the line with packs between stations and show how their incomplete records are handled on restart. Separate instrument results from final disposition in the production record so a reported failure can be traced to the actual pack response. Record the test cases in the integration specification checklist.
Line connections can change the approach for Combination Inspection Systems
- A camera can only assess a property made visible and repeatable by the inspection setup.
- Sample diversity and marginal cases determine how meaningful a feasibility result is.
- Visual inspection does not replace hidden, destructive, functional or statutory tests.