A combination inspection system connects several checks to the same product. Vision, code reading and weight measurement answer different questions; a useful design keeps those results distinct while controlling the correct pack when any required check fails.
Speak directly with Oxford Vision Systems about combined vision, code and weight inspection.
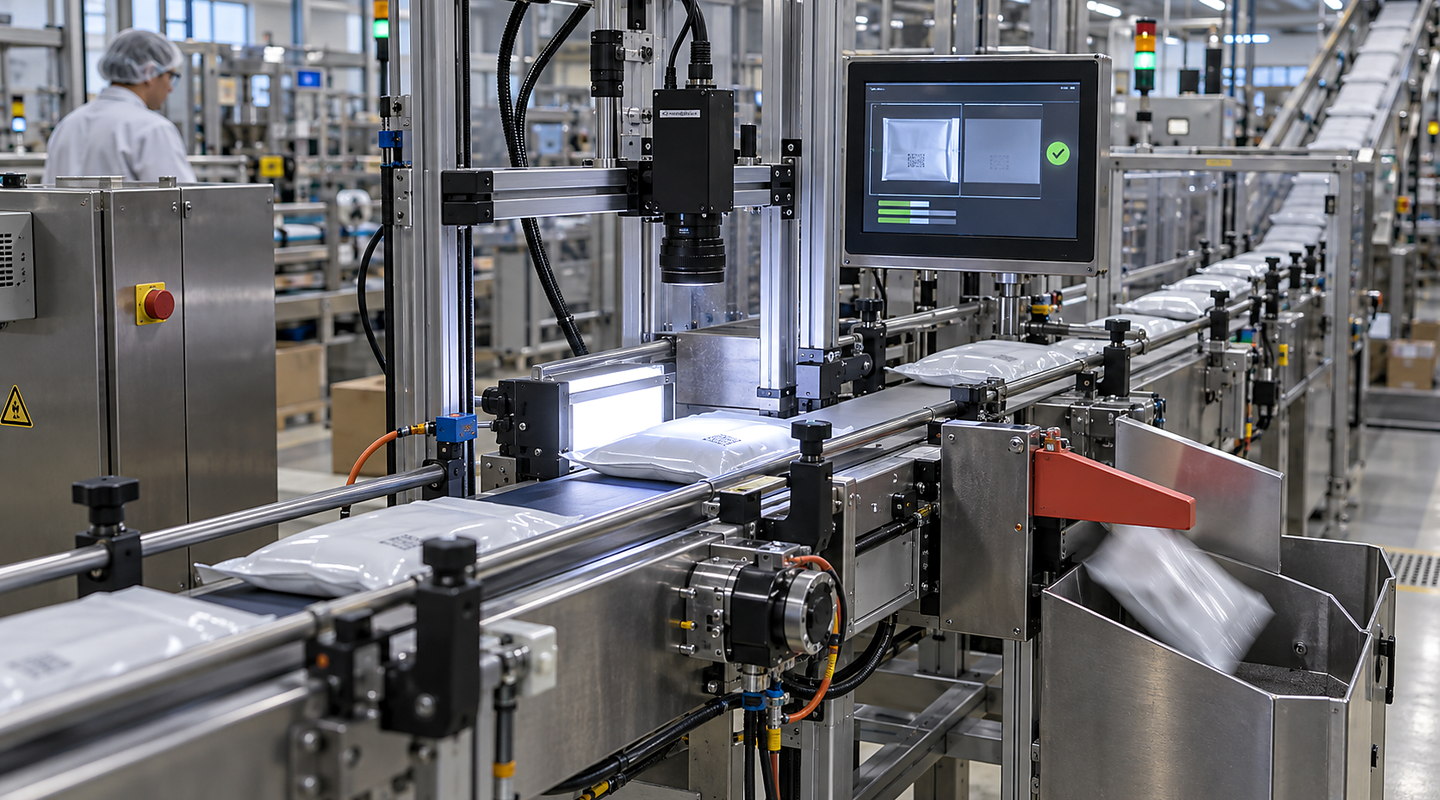
Photographs illustrate general inspection equipment. Combined vision, code and weight performance must be established with representative packs and the complete result and reject sequence.
Quick answer
When should we combine vision, code checks and weighing in one inspection station?
List the decision each inspection must make and the product identity shared between them. Define what happens when one check fails, a result is missing or a pack cannot be tracked. Trial the combined sequence and reject confirmation so that several instruments produce one controlled decision about the correct pack.
Application decisions
Make several inspection results one controlled pack decision
Decision 1
Define the decision at each instrument
Write a separate acceptance rule for appearance, code content and weight. Identify which defects each instrument can detect and which remain outside scope. This avoids treating a successful barcode read or a correct gross weight as proof that the whole pack is acceptable.
Decision 2
Preserve product identity between checks
Describe how packs are triggered and tracked from the first inspection to the reject point. Include stops, variable gaps and packs removed from the conveyor. Challenge whether a late result can be accidentally assigned to the next product.
Decision 3
Coordinate recipe changes
Identify the source of the approved product code, weight limits and vision recipe. Agree how every instrument confirms the requested setup before production resumes. A valid measurement made against the wrong product recipe is still an incorrect inspection decision.
Decision 4
Separate failed, missing and uncertain results
Specify the response to a definite failure, a no-read, a timed-out result and loss of communication. These states need explicit handling rather than silently becoming a pass. Decide which events call for rejection, segregation or a controlled line stop.
Decision 5
Confirm physical rejection
Define how the rejected pack is controlled and how removal is confirmed. Include a full reject area, consecutive failed packs and loss of the reject device’s services in the challenge plan. A reject command alone is not evidence that the intended product left the accepted stream.
Decision 6
Retain useful reasons and records
Keep the instrument result and the final pack decision associated in the production record. This lets quality teams distinguish a weight trend from a code or presentation fault. Use the inspection integration guide to define result and line-control interfaces.
A new station can define the presentation from the outset; a retrofit must work within existing transfers, space and control ownership. Both need an agreed association between the product and every inspection result.
List each unacceptable condition and the inspection expected to identify it.
02
Prove each method separately
Use representative acceptable, faulty and marginal packs to establish the limits of every check.
03
Challenge the joined sequence
Test tracking, delayed results, recipe changes and consecutive rejects under the intended line conditions.
04
Review the final product record
Confirm that the accepted or rejected pack can be matched to its individual inspection results.
Important limits
Know what needs a separate check
A camera can only assess a property made visible and repeatable by the inspection setup.
Sample diversity and marginal cases determine how meaningful a feasibility result is.
Visual inspection does not replace hidden, destructive, functional or statutory tests.
Your final solution for combined vision, code and weight inspection must reflect the law, current standards and site-specific risks that apply to your installation.