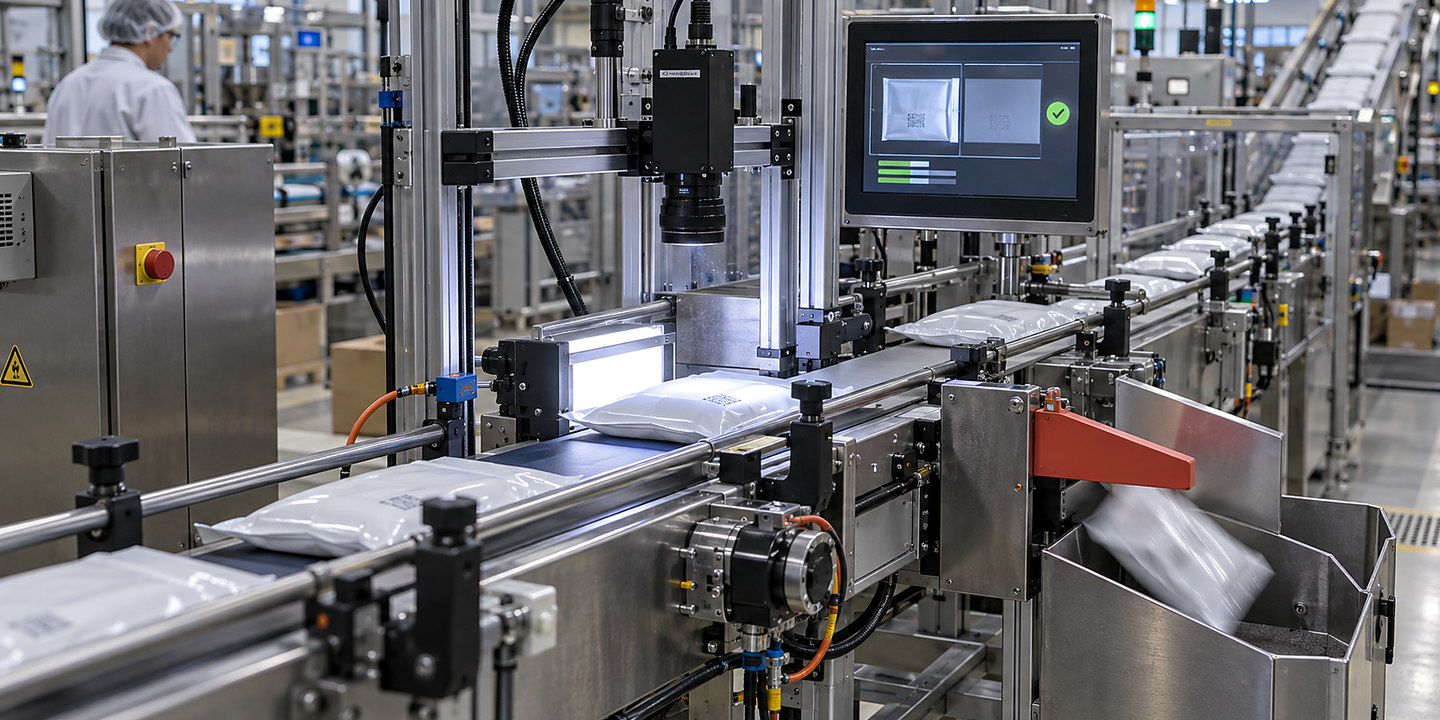
Photographs illustrate general inspection equipment. Combined vision, code and weight performance must be established with representative packs and the complete result and reject sequence.

In brief

Choose an approach to combination inspection systems by what the product or part does in production and by the result you need—not by sector name alone.

For in-line inspection using combined vision, code and weight inspection and retrofit or multi-variant checks involving combined vision, code and weight inspection, different operating conditions can change the recommended approach.

On the production floor

Match the solution to your product, part and operating needs — Combination Inspection Systems

Plan combination inspection systems around representative good, bad and marginal samples, line presentation, lighting, reject handling and challenge criteria. Discuss an optical feasibility trial with Oxford Vision Systems. Use the application examples to compare in-line inspection using combined vision, code and weight inspection with retrofit or multi-variant checks involving combined vision, code and weight inspection.

Discuss your application
Application 1

In-Line Inspection Using Combined Vision, Code and Weight Inspection

For in-line inspection using combined vision, code and weight inspection, start by confirming visible defect or measurement definition for combined vision, code & weight inspection, good, bad and marginal sample range, and part presentation and production speed so the proposed system matches your real production needs.

Explore this application
Application 2

Retrofit or Multi-Variant Checks Involving Combined Vision, Code and Weight Inspection

For retrofit or multi-variant checks involving combined vision, code and weight inspection, start by confirming good, bad and marginal sample range, part presentation and production speed, and optics, lighting and environmental conditions so the proposed system matches your real production needs.

Explore this application
Choose the right route

Four questions that can change the recommended approach

What arrives?

Describe the real range for visible defect or measurement definition for combined vision, code & weight inspection and good, bad and marginal sample range, plus presentation and upstream controls—not just a nominal drawing.

What must happen?

Define the required outcome for in-line inspection using combined vision, code and weight inspection, the allowed window and what your team can recover without outside help.

What surrounds it?

Record the space, services, neighbouring equipment, people, cleaning and data connections around retrofit or multi-variant checks involving combined vision, code and weight inspection.

What result do you need?

Agree representative trials, difficult samples and the result record for false-accept, false-reject and challenge criteria, including who will review it.

ApproachOften suitable whenWatch for
Combination Inspection SystemsYou need a dedicated solution for a clearly defined duty, product or part range and line interface.A camera can only assess a property made visible and repeatable by the inspection setup.
Purpose-Built Sensors for Simple Presence or Position ChecksThe required decision is a simple presence or position check that representative trials can demonstrate.Confirm the detection scope and presentation range; a presence check does not establish appearance, code content or weight acceptance.
Offline Metrology or Destructive Tests where the Property Is Not Visible InlineThe required property cannot be established by the available in-line inspection methods.Specify the separate test and acceptance evidence; a combined inspection result does not replace hidden, destructive, functional or statutory checks.